
Heat-sealing equipment designed for large-scale membrane structure projects—such as sports venues and canopies—must meet three core requirements: large-format processing capabilities, high-strength welding, and high-precision control. The following outlines professional-grade equipment selection and technical specifications:
**I. Classification of Specialized Heat-Sealing Equipment for Large-Scale Projects**
1. **Gantry-Type High-Frequency Welding Machine**
**Core Advantages:**
Ultra-wide processing capability (welding bar length: 1.5–20 m); enables single-pass welding of long seams (e.g., stadium roof ridges)
Dual-head synchronous welding increases efficiency by 40% (e.g., 12 m seam in ≤8 minutes)
**Key Technologies:**
Constant pressure system (adjustable 0.3–0.7 MPa; ±1% tolerance)
Infrared temperature control (180–220°C ±2°C)
**Applicable Materials:** PVC-coated polyester fabric, PTFE-coated fiberglass membrane
2. **Intelligent Heat-Press Welding System**
**Design Features:**
Modular heating plates (single unit 1×3 m; extendable up to 30 m)
Layered temperature control technology (ETFE membrane: 300°C ±5°C; PVC membrane: 200°C ±5°C)
**Typical Applications:**
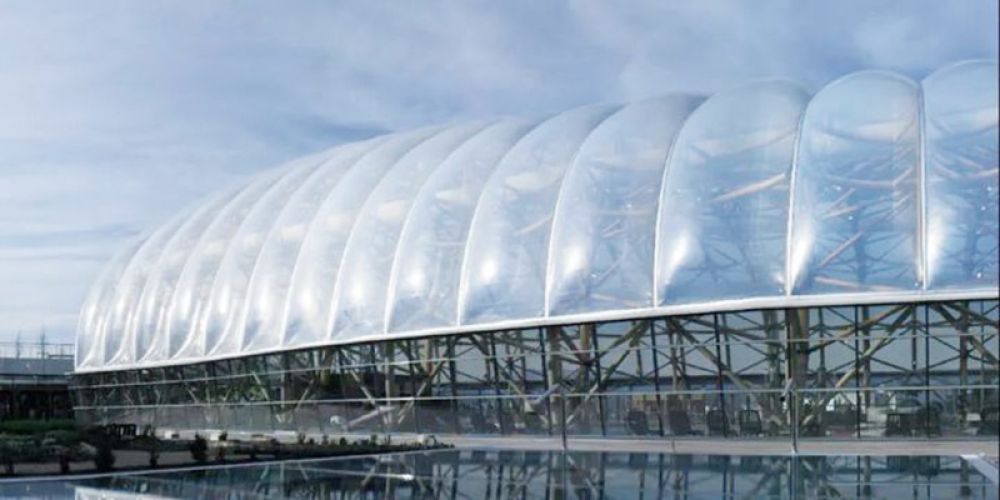
Beijing Daxing Airport ETFE cushions (welding area ≥50 m² per cushion)
Qatar World Cup stadium shading roofs
3. **Mobile On-Site Welding Platform**
**Functional Innovations:**
Hydraulic lifting mechanism (working height: 0–25 m); adaptable to curved roof construction
Laser projection positioning (seam precision: ±1 mm/10 m)
**Representative Model:**
Leister VARIMAT V2 (Germany) – integrates hot-air and extrusion welding functions
**II. Comparison of Key Technical Parameters for Large-Project Equipment**
**Equipment Type** | **Processing Dimensions** | **Welding Strength (MPa)** | **Energy Consumption (kW)** | **Applicable Membrane Thickness**
Gantry High-Frequency Welder | Width 1.5–20 m × Length ∞ | ≥24 (PVC) | 25–100 | 0.8–3.0 mm
Modular Heat-Press Machine | Single module 1×3 m (expandable) | ≥28 (ETFE) | — | — 40–200 0.05–0.5 mm
Mobile welding platform Curved surface adaptive ≥18 (repair welding) 15–30 0.5–2.5 mm
Note: Welding strength testing standards refer to EN ISO 1421 (membrane peel strength ≥98% of base material).
III. Technical Analysis of Project Cases
Case 1: Jeddah Stadium, Saudi Arabia (PTFE membrane roof)
Equipment: 32-meter gantry high-frequency welding machine
Process:
Double-layer PTFE membrane (1.2 mm + 1.0 mm)
High-frequency parameters: Power 65 kW, pressure 0.5 MPa, duration 90 seconds/meter
Result: Weld airtightness ≤0.03 m³/m²/h (passed hurricane test)
Case 2: Marina Bay Sunshade, Singapore (ETFE pneumatic cushions)
Equipment: Heat-press welding system (assembly of 12 modular units)
Process:
Three-layer ETFE membrane (0.25 mm × 3)
Gradient heating: 250°C (bottom layer) → 200°C (middle layer) → 180°C (top layer)
Result: Light transmission uniformity error ≤2% (10-year maintenance-free)
IV. Key Factors for Equipment Selection
Membrane Material Characteristics:
PVC/PTFE → High-frequency welding preferred (good response from polar molecules)
ETFE → Heat-press welding mandatory (non-polar material requires contact heat conduction)
Structural Complexity:
Double-curvature roof (e.g., cable dome) → Mobile welding platform + 3D scanning positioning
Flat, long-span structure → Gantry high-frequency machine (30% cost reduction)
Membrane material heat-sealing technology is a critical process in the fabrication of membrane structures, primarily relying…
Heat-sealing equipment designed for large-scale membrane structure projects—such as sports venues and canopies—must meet three core…
In the sealing of inflatable structures, the heat-sealing process fuses material contact surfaces through high-temperature heating…
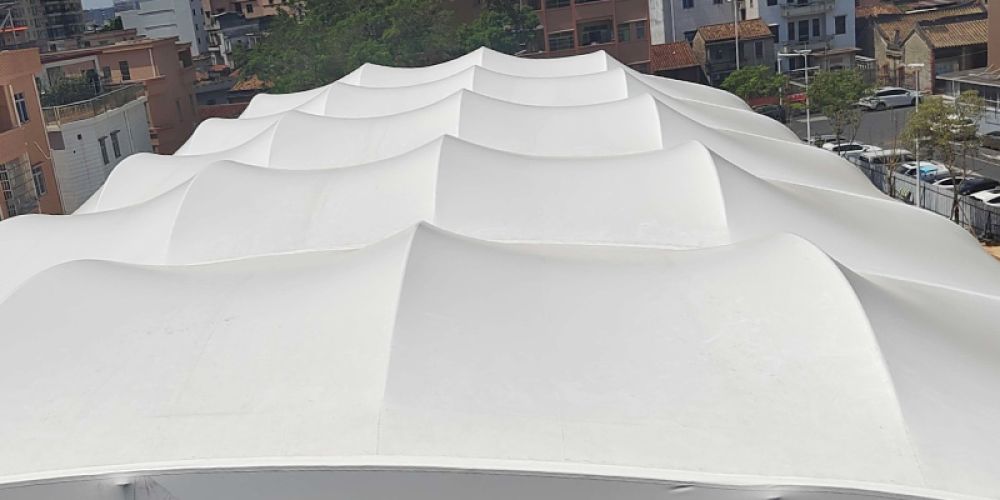
In the field of architecture, various new membrane materials are widely used due to their unique…
In the construction field, the heat-sealing production methods for different new membrane materials vary depending on…
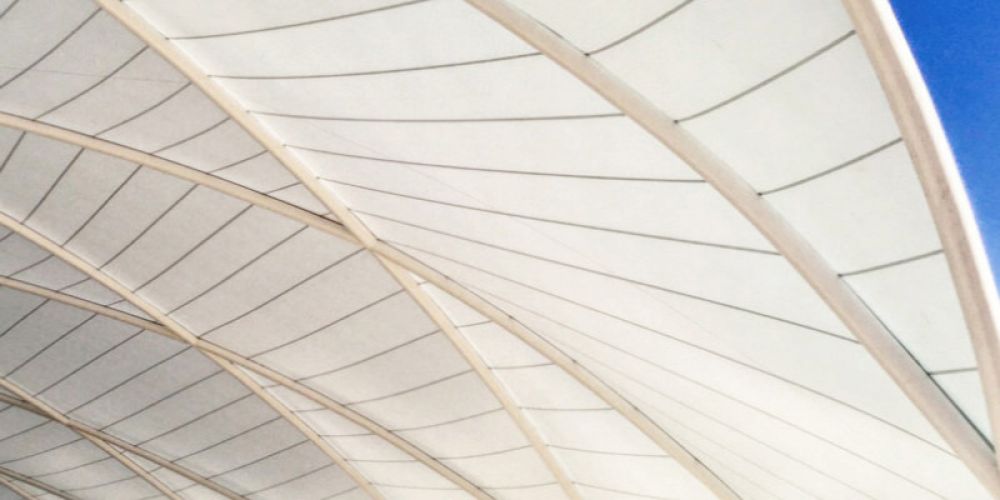
In the construction field, the heat-sealing of PVDF membrane materials is mainly achieved through processes such…